
In today’s competitive manufacturing and distribution environment, product packaging plays an important role in product protection, presentation, storage and transportation. Businesses need packaging materials that not only protect products but also improve handling efficiency, maintain product quality and create a professional appearance.
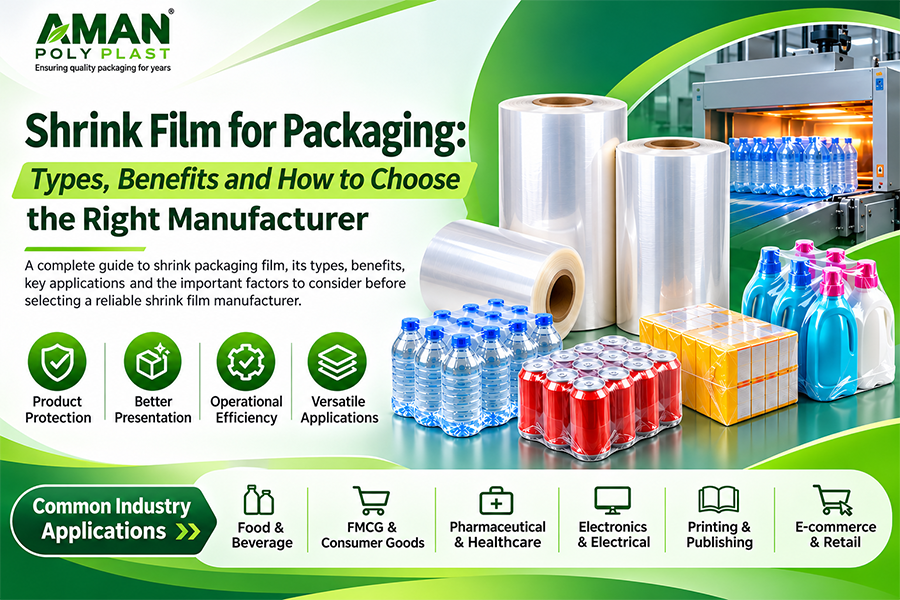
Shrink Film is one of the widely used flexible packaging solutions across manufacturing, food processing, retail, e-commerce, FMCG and industrial sectors. It is a polymer-based plastic film that shrinks tightly around a product when exposed to controlled heat, creating a secure and protective covering.
Depending on the application, manufacturers use different types of Shrink Packaging Film, including Polyolefin (POF), Polyethylene (PE) and PVC shrink films.
A suitable Heat Shrink Film provides a close-fitting finish around products, helping protect them from dust, moisture exposure, scratches, handling damage and external contamination, depending on the material specification and packaging conditions.
Why Is Shrink Film Important for Businesses?
Businesses increasingly prefer shrink packaging because of its versatility, operational convenience and ability to accommodate products of different shapes and sizes.
Key advantages include:
- Product Protection: Helps protect products against dust, dirt, scratches and external handling during storage and transportation.
- Improved Product Presentation: Provides a neat, transparent and professional packaging appearance.
- Secure Packaging: Creates a tight covering that helps keep products together during handling and distribution.
- Storage Efficiency: Suitable for individual product packaging as well as multipack and bundle packaging.
- Operational Flexibility: Available in different thicknesses, widths and formats to suit various packaging requirements.
- Brand Visibility: Transparent shrink films allow customers to view the packaged product without opening the packaging.
- Versatile Applications: Suitable for packaging consumer goods, industrial products, food multipacks, printed materials and many other products.
Choosing the right Shrink Film for Packaging is therefore not simply about purchasing plastic film. It is about selecting a packaging solution that matches your product, machinery, production capacity and distribution requirements.
Who Needs Shrink Packaging Film? Industries and Business Applications
Shrink packaging is used across a wide range of industries. Manufacturers, distributors and packaging companies require different film specifications depending on the product type, packaging machinery and intended application.
Industries That Benefit from Shrink Film Packaging
Shrink film is a versatile packaging material widely used across industries that require secure product bundling, improved presentation and protection during storage, handling and transportation. From food and beverage manufacturers packaging water bottles, soft drinks and snack multipacks to FMCG companies wrapping personal care, household and cleaning products, shrink packaging offers an efficient solution for different product categories. Pharmaceutical and healthcare businesses use it for secondary packaging of medicine cartons, hygiene products and medical supplies, while electronics and electrical manufacturers use it for packaging accessories, cables, components and small appliances. Similarly, printing and publishing companies rely on shrink wrap rolls to bundle books, magazines, notebooks and stationery products. E-commerce businesses, retailers and distribution companies also benefit from shrink packaging for promotional bundles, gift sets, multipacks and distribution-ready products. With its flexibility, adaptability and availability in different material specifications, shrink film serves as a practical packaging solution for businesses across manufacturing, retail and distribution sectors.
What Should You Consider Before Buying Shrink Film?
Selecting the right shrink film supplier is essential for maintaining packaging quality, production efficiency and cost-effectiveness. Although low-cost film may seem attractive, inconsistent quality, machine downtime, material wastage and delayed deliveries can increase overall operational costs. Before purchasing a Shrink Wrap Film Roll, businesses should evaluate the following factors.
A. Film Quality and Technical Specifications
Film quality directly influences packaging performance, product protection and appearance. Before purchasing, consider the required film thickness (micron), width, roll dimensions and shrinkage percentage according to your product and machinery requirements. Also evaluate tensile strength, puncture resistance, transparency, gloss and sealing performance to ensure consistent packaging results. Batch-to-batch quality consistency is equally important to minimise production defects and material wastage.
B. Supply Chain, Production Capacity and Delivery Reliability
A dependable Shrink Film Manufacturer should have sufficient production capacity and a reliable supply chain to fulfil regular and seasonal business requirements. Evaluate raw material availability, manufacturing lead times, bulk-order capabilities and inventory management to avoid production interruptions. Also consider the supplier’s geographical reach, delivery schedules, communication and ability to accommodate customised requirements such as different film widths, thicknesses and roll lengths. Reliable after-sales and technical support can further strengthen long-term supplier relationships.